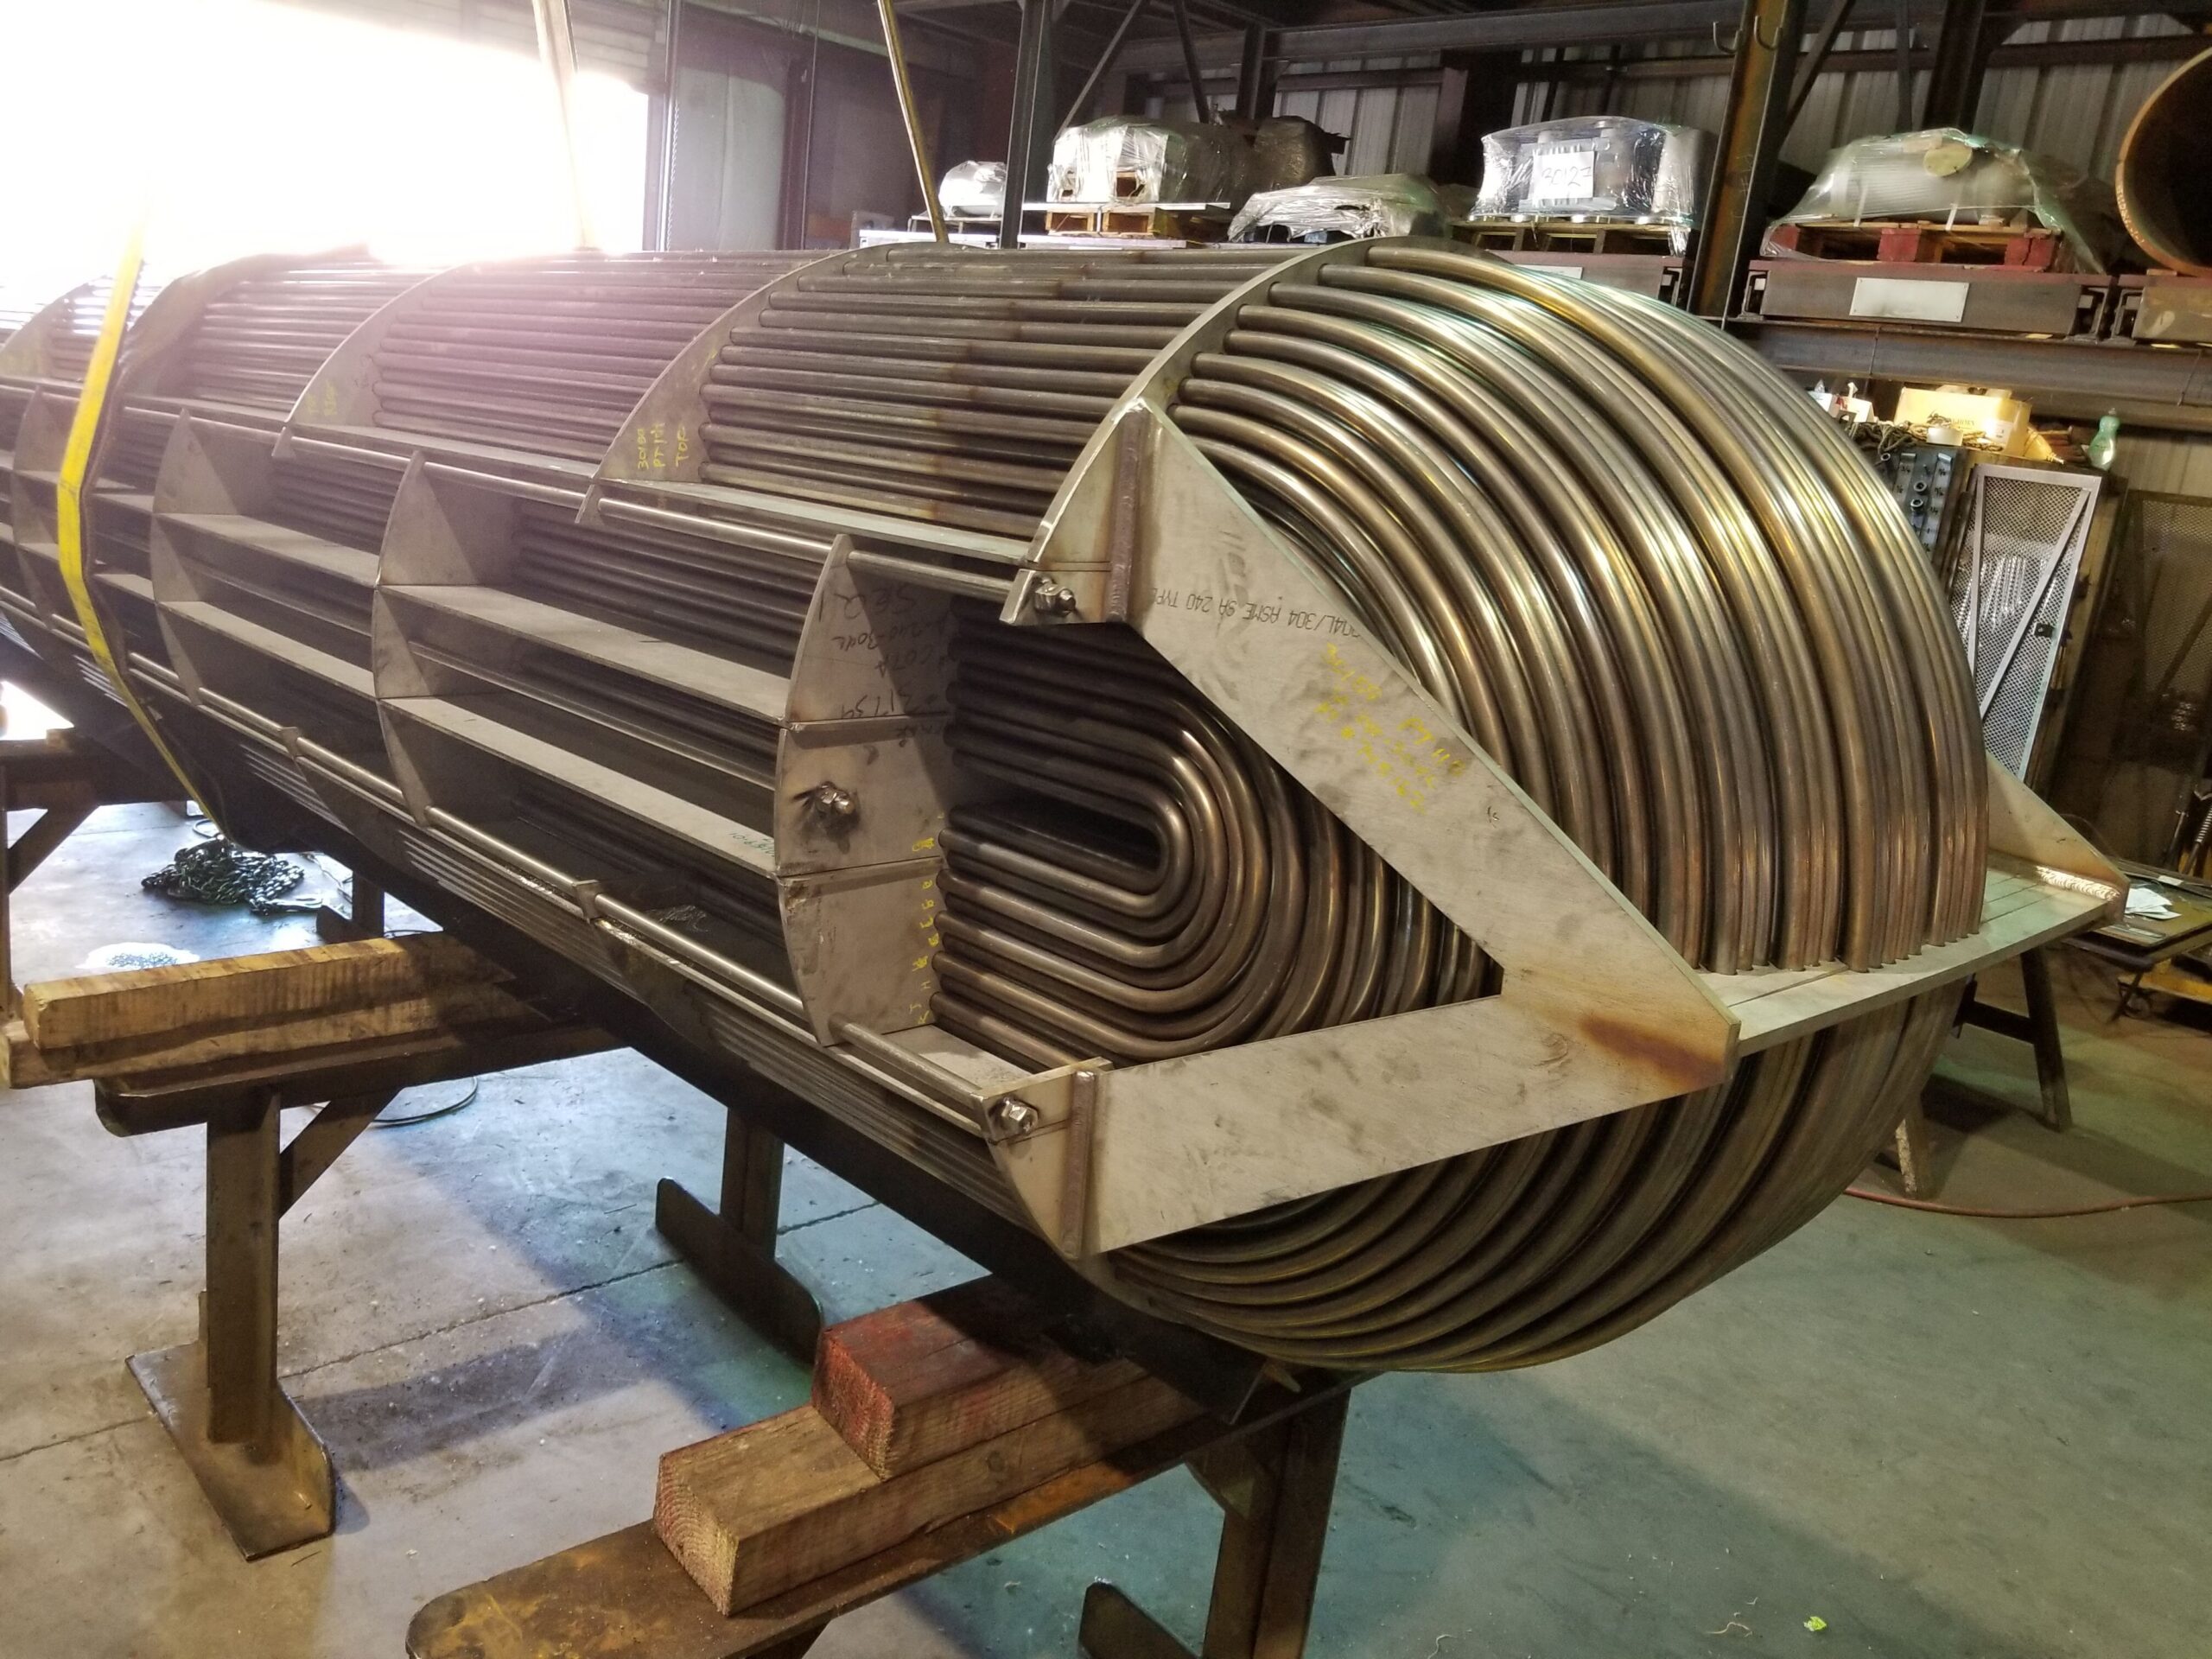
Fertilizer production and clean hydrogen synthesis place extraordinary demands on industrial process equipment. In these energy-intensive facilities, heat exchangers have to handle substantial heat loads while withstanding corrosive chemicals, high temperatures, mechanical stress, and demanding pressures.
Selecting the wrong alloy can accelerate corrosion and lead to tube sheet deformation, pinhole leaks, unplanned shutdowns, and serious safety hazards.
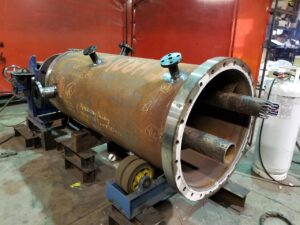
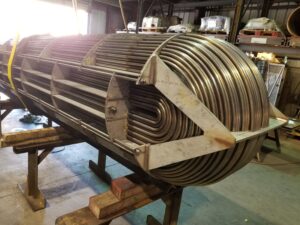
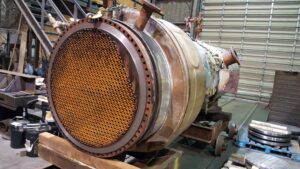
At Enermax, we combine decades of metallurgical and engineering experience to custom-engineer shell and tube heat exchangers, pressure vessels, and specialized thermal systems for demanding process environments. The sections below look at common failure mechanisms and explain how alloy selection can affect equipment life, compliance, and overall reliability.
Many modern chemical facilities put conventional metals under demanding combinations of pressure, temperature, and chemical exposure. Ammonia, urea, and hydrogen synthesis expose equipment to aggressive chemicals, high pressures, and significant temperature fluctuations. Equipment failure can interrupt connected operations, create safety risks, and generate substantial financial losses.
Fertilizer manufacturing involves volatile compounds including synthetic ammonia, urea, nitric acid, and ammonium nitrate. During urea production, ammonium carbamate forms under elevated temperature and pressure and is extremely aggressive toward carbon steel and conventional 300-series stainless steels.
If the alloy is not suited to the process, carbamate can break down the protective passive film on internal surfaces. Over time, that can lead to wall thinning, pitting, and early component failure.
Chemical and clean-energy processes can cycle between cryogenic conditions and temperatures exceeding 1,000°F (538°C). Repeated heating and cooling cause different rates of expansion and contraction between the exchanger shell, tubes, bundle, and tube sheet.
Because the components expand and contract at different rates, mechanical stresses can develop around tube-to-tubesheet connections and welded joints. Repeated cycling may eventually lead to relaxation, cracking, fatigue, or damage to the tube bundle.
Hydrogen generation, syngas loops, and fertilizer synthesis systems can operate at sustained pressures ranging from 2,000 PSI to more than 5,000 PSI.
Because hydrogen molecules are exceptionally small, they can diffuse into microscopic defects within susceptible metals. Long-term exposure can contribute to stress cracking, creep deformation, and changes in the metal’s microstructure. Material selection and fabrication controls therefore need to be considered carefully.
A lower purchase price does not necessarily mean a lower overall cost. Equipment that is poorly matched to the process may require more maintenance, earlier repairs, or premature replacement.
Investing in corrosion-resistant materials during the design stage remains one of the most effective ways to protect production and extend equipment service life.
The alloy needs to be selected around the actual process chemistry. Depending on the application, that may mean conventional stainless steel, duplex or super duplex grades, or a nickel-based alloy.
Cooling water and process fluids can contain dissolved chlorides. Conventional 300-series stainless steels, including 304/304L and 316/316L, are vulnerable to chloride stress corrosion cracking when tensile stress and temperatures exceed approximately 140°F (60°C).
Chloride SCC can produce branching cracks that penetrate the alloy without obvious surface corrosion, potentially resulting in sudden pressure-boundary failure.
To improve resistance, equipment manufacturers may specify:
Urea production requires stable passive-film protection on exposed metal surfaces. When dissolved oxygen levels fall in ammonium carbamate process loops, corrosion of conventional stainless steels can accelerate.
Urea-grade austenitic alloys, such as 316L Modified and 25-22-2 / UNS S31050, are designed to maintain passive protection under oxygen-depleted, high-pressure carbamate conditions.
Increasing tube-wall thickness can provide additional corrosion allowance, but it also increases thermal resistance and equipment weight. High-strength duplex and super duplex alloys can allow engineers to use thinner walls while maintaining structural safety factors.
Using a stronger alloy can therefore allow a thinner wall without giving up the required safety margin, while also limiting the effect of added material on heat transfer and equipment weight.
Because hydrogen atoms are so small, they can diffuse into certain steels. In hydrogen-service equipment, that makes both material choice and fabrication practices important considerations. In hydrogen-service heat exchangers, improper materials or fabrication procedures can therefore contribute to brittle failure.
Hydrogen-related degradation can occur through two primary mechanisms:
Material selection for hydrogen service should follow the Nelson Curves in API RP 941, which establish safe operating boundaries based on temperature and hydrogen partial pressure.
Weld seams and heat-affected zones (HAZ) can be particularly susceptible to hydrogen-related damage because of residual stresses and localized metallurgical changes.
Reliable fabrication requires:
The initial fabrication price tells only part of the cost story. Maintenance, replacement, inspection, and lost production can have a much larger effect over the equipment's service life. Application-specific alloys can provide substantial lifecycle benefits.
Carbon steel and lower-grade stainless steel bundles exposed to corrosive fluids may require frequent NDE, tube plugging, chemical cleaning, and premature replacement.
High-performance alloys can extend inspection and replacement intervals, reducing maintenance labour and helping shorten planned turnarounds.
Corrosion products and surface scale can create an insulating layer on heat exchanger tubes, reducing heat-transfer performance over time. Using a corrosion-resistant material can limit the buildup that interferes with heat transfer, helping the exchanger maintain its performance for longer.
Standard process equipment may not withstand the combined thermal, chemical, and mechanical demands of modern fertilizer and hydrogen facilities. Severe-service applications require custom equipment engineered to specific process conditions, mechanical codes, and project requirements.
When selecting a custom manufacturing partner, verify that they maintain the following capabilities:
Severe-service heat exchangers require more than basic fabrication. Material selection, mechanical design, welding, fabrication controls, and inspection all have to work together.
At Enermax, we bring decades of custom design and fabrication experience to shell and tube heat exchangers, pressure vessels, and specialized thermal systems engineered for fertilizer production and high-pressure hydrogen service.
Enermax supports projects at different stages, from new facility development and process debottlenecking to tube-bundle replacement. Our engineers can assist with thermal analysis, mechanical modelling, NDT, fabrication, and final delivery.
Contact us to discuss your process parameters, fluid chemistry, operating conditions, and custom heat-transfer requirements with our engineering specialists.
Talk to an engineer
Send us your drawings or specifications and we will come back with a fabrication approach and a realistic timeline.
Request a QuoteOr call
604 924 7232Certified to
Every vessel and exchanger we build starts with your process conditions, not a catalogue page. Send us the duty and we will tell you what it takes to make it.
Fabricated in Maple Ridge, BC.
Written by
Enermax Mountain Manufacturing designs, fabricates and repairs ASME Section I and Section VIII Div. 1 heat exchangers, pressure vessels, and ASME B31.1 and B31.3 industrial piping from its shop in Maple Ridge, BC.
Talk to our team →