
Engineering Sulphur Condensers for the Modern Refinery
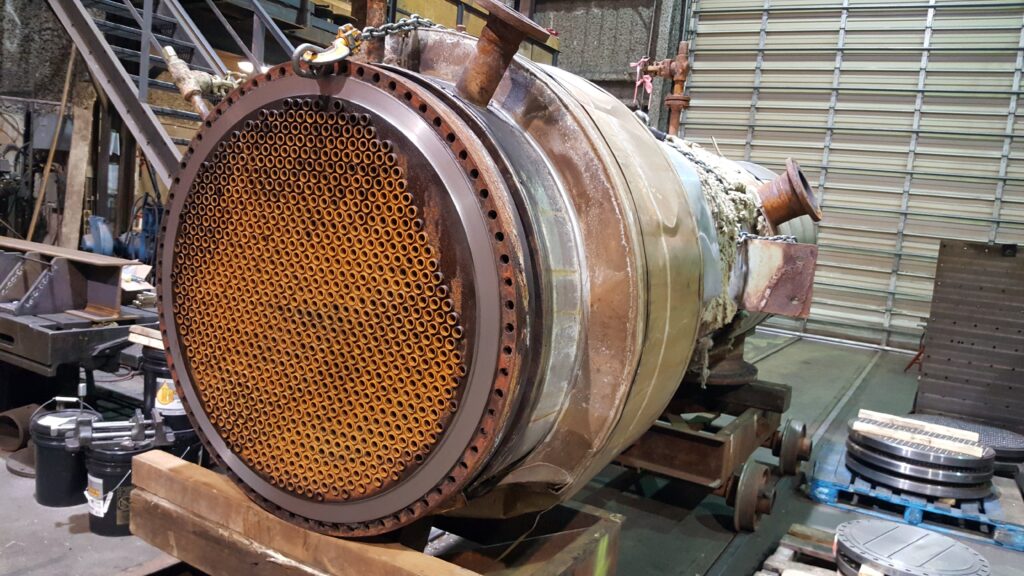
Sulphur recovery is a critical phase in modern oil and gas refining. Environmental mandates require facilities to extract elemental sulphur efficiently before processing finishes. At the heart of this process is the sulphur condenser, a highly specialized industrial heat exchanger. Managing these thermal demands requires a deep understanding of chemical engineering, precise manufacturing, and strict […]
Maximizing Plant Efficiency with BFW Blowdown and Boiler Heat Recovery
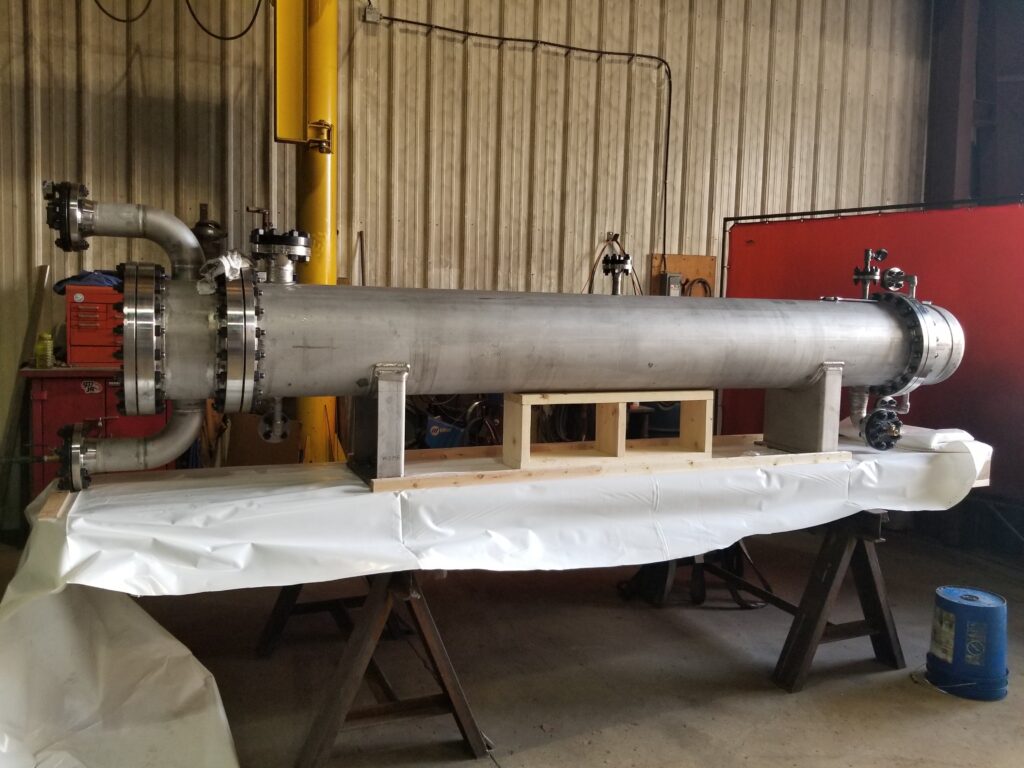
Industrial boiler systems are the heart of many Canadian facilities, but they are also significant sources of energy loss. One of the most effective ways to reclaim this lost energy is through a boiler heat recovery system. By capturing thermal energy that would otherwise be discarded, plants can significantly lower fuel costs and reduce their […]
Top Benefits of Shell and Tube Heat Exchangers in Industrial Applications
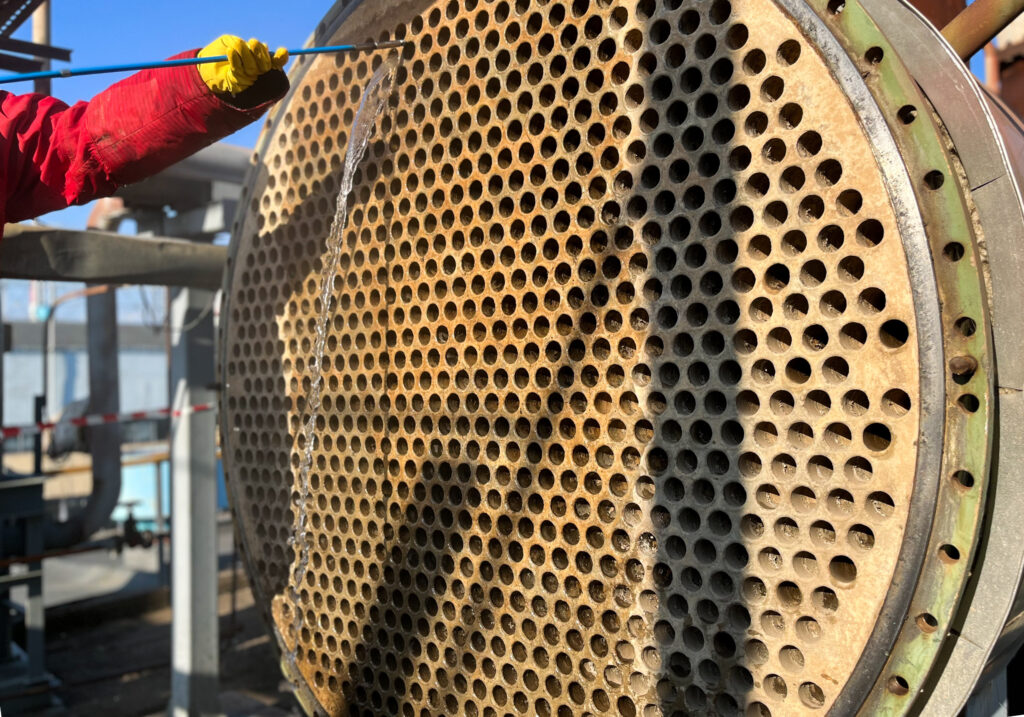
Efficient heat transfer is vital to industrial performance, safety, and energy use. Across industries from manufacturing to energy, shell and tube heat exchangers lead the way. Known for their flexibility, durability, and efficiency, they’ve become a go-to solution for reliable thermal management in demanding industrial environments. What is a Shell and Tube Heat Exchanger? A […]
How Shell and Tube Heat Exchangers Work: Explained for Engineers and Buyers

Shell and tube heat exchangers are used for efficient heat transfer in industrial applications, from oil refining to HVAC. Despite their complex appearance, they operate on a simple principle. Let’s review the basics if you want to understand, select, or specify the right exchanger for your needs. How It Works: The Basics At the core […]